Explore our turnkey product portfolio and high-tolerance primary containers engineered for barrier-integrity, precise dosing, and retail-shelf compliance.
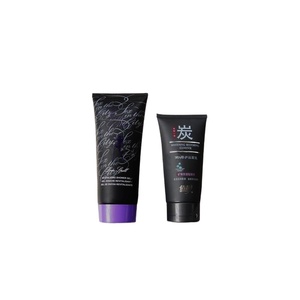
Cosmetic tube packaging demands absolute synchronization between bulk rheology and mechanical volumetric dispensing. Our automated lines combine ultrasonic hermetic sealing with zero-drip nozzle cut-offs to eliminate seal contamination.
We configure dual-mode tail sealing (Hot-Air contact for standard polyethylene, and High-Frequency Ultrasonic for composite laminated substrates). This prevents polymer stress cracking while ensuring 100% burst test containment for retail distribution.
Viscous shearing causes aeration and foaming in rich keratin emulsions and peptide gels. Our custom servo-driven bottom-up filling nozzles eliminate cavitation, stringing, and micro-voids, guaranteeing volumetric uniformity down to ±0.5% margin.
Every tube batch runs through continuous electronic batch records (eBR). Real-time optical sensors detect lot code integrity, visual orientation, and crimp defects, upholding full compliance with U.S. FDA MoCRA and EU No 1223/2009 standards.
Selecting the correct tube barrier ensures active compound viability across long global transit lines. We match formulation viscosity to structural resins.
| Tube Substrate Format | Barrier Properties (OTR / WVTR) | Typical Applications | Sealing Technology | Compliance Rating |
|---|---|---|---|---|
| Mono/Double-Layer PE (LDPE, HDPE) | Standard Moisture Resistance; Moderate O2 Permeability | Daily Cleansers, Body Washes, Basic Hand Lotions | Direct Thermal / Hot-Air Crimp | FDA GRAS • REACH |
| 5-Layer Co-Ex EVOH | Ultra-Low Oxygen Transmission (<0.5 cc/m²·day) | Exosome Serums, Retinol, Glabridin Actives, Vitamin C | High-Frequency Ultrasonic Sealing | ISO 22716 • cGMP |
| ABL (Aluminum Barrier Laminate) | Absolute Gas, Light, & Volatile Fragrance Barrier | Pharmaceutical Ointments, Hair Dyes, Depilatories | High-Frequency Induction Welding | EU 1223/2009 • USP |
| PBL (Plastic Barrier Laminate) | High Elasticity (Anti-Dent Memory), Moderate-High Barrier | Premium Skincare Serums, Keratin Leave-In Masks | Rotary Hot-Air with Edge Trimming | MoCRA Certified |
| PCR Polyolefin (Post-Consumer) | Eco-Certified Sustainable; 30%–100% Recycled Content | Vegan Lip Balms, Organic Shampoo, Eco Hair Treatments | Modified Temperature Controlled Hot-Air | Global Recycled Standard |
The global contract packaging ecosystem is pivoting toward closed-loop circular packaging, airless pump-tube fusions, and clean-formula barrier resilience. Procurement heads must anticipate the following structural shifts:
Traditional tubes with mixed PE bodies and PP flip-top caps complicate regional recycling. Procurement is shifting rapidly toward 100% mono-material HDPE assemblies (sleeve, shoulder, and cap) allowing seamless curbside recycling stream reclamation.
As complex bio-ferments, exosomes, and un-stabilized peptides replace standard cosmetics, tubes must provide absolute EVOH micro-barrier shielding against photo-oxidation without heavy metal leaching.
Brands increasingly demand tubes with cold-touch ceramic tips, medical-grade silicone brush heads, and stainless steel micro-rollers directly clamped to the tube neck, eliminating secondary application tools.
Global procurement teams prioritize turnkey providers who handle primary blow-molding/extrusion, contract bulk compounding, automated filling, and international MoCRA regulatory dossiers in one consolidated facility.
By unifying cleanroom compounding, in-house high-tolerance tube filling, and empirical on-site testing under a single quality audit framework, we eliminate intermediary hand-off risks.
Critical operational answers for brand owners, supply chain managers, and contract packaging directors.
For custom tube filling utilizing in-stock tube tooling, MOQs begin at 2,500 units for standard skin and hair care sizes (2.1 oz to 8 oz). For fully custom extruded tube sleeves featuring pantone-matched coloration, silk-screen printing, or specialized metallization, standard MOQs typically start at 10,000 units due to industrial extrusion run minimums.
We employ positive displacement rotary piston pumps paired with diving nozzles that execute bottom-up volumetric filling. By controlling the withdrawal rate of the nozzle relative to the fluid level and utilizing positive vacuum cut-off valves, we prevent product tailing, nozzle dripping, and trapped air cavities within non-Newtonian bulk formulas.
Initial R&D prototype batches take approximately 2 to 4 weeks. Following bulk formula and packaging component sign-off, commercial contract compounding, filling, automated tail-coding, QC quarantine testing, and pack-out require 4 to 8 weeks, depending on component availability and international regulatory registration workflows.
Yes. Under our contract manufacturing agreements, clients may supply their own custom-printed empty tubes or ship bulk bulk-concentrates for toll filling. We conduct thorough incoming packaging inspection (dimensions, wall thickness, seal zone contamination) and laboratory compatibility analysis before scheduling production line runs.
Every production run undergoes destructive burst pressure testing, vacuum chamber dye penetration analysis to detect micro-capillaries, and torque release evaluation of the orifice closure. High-temperature (45°C) inverted oven stability is checked over 72 hours to ensure active lipids or surfactants do not degrade polymer weld boundaries.
Our facilities maintain full compliance with the Modernization of Cosmetics Regulation Act (MoCRA), providing verified facility registration numbers, product formulation listings, full quantitative breakdown of active compounds, microbiological release certificates, and standard Certificate of Free Sale (CFS) document management.
Connect directly with our engineering specialists. Review line tooling capabilities, request pilot samples, or discuss custom bulk formulation specs with an expert today.
Contact Us